Featured Industrial Rack & Storage Shelf Systems
Engineered to ISO 9001, FEM 10.2.02, RMI, and ABNT NBR 15524 standards. Built with premium cold-rolled Q235B and Q355B structural steel for maximum dynamic payload stability.
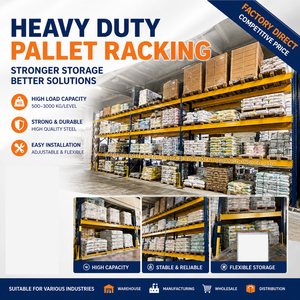
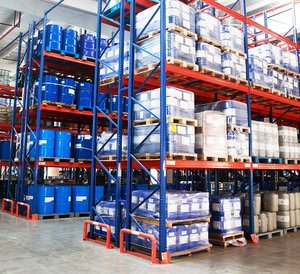
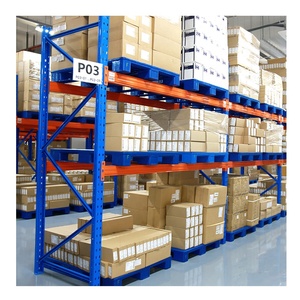
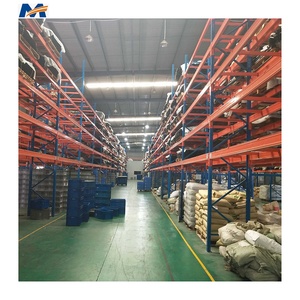
Navigating Industrial Storage Engineering: A Definitive Sourcing Guide for Global Buyers
In the rapidly evolving landscape of global supply chain management, selecting the appropriate rack storage shelves manufacturer and exporter in China is a critical strategic decision. Industrial warehouse storage is no longer merely about static steel frames; it is an engineered ecosystem directly influencing cubic space utilization, throughput speed, structural safety compliance, and long-term operational expenditure (OPEX).
Modern logistics facilities demand stringent structural design standards. From handling standardized European pallets (800 × 1200 mm) and American GMA pallets (48 × 40 inches) to specialized Brazilian PBR pallets (1000 × 1200 mm), storage infrastructure must withstand multi-ton static loads and dynamic impact forces from MHE (Material Handling Equipment) such as reach trucks, VNA (Very Narrow Aisle) forklifts, and AGVs (Automated Guided Vehicles).
As a premier Chinese manufacturer with decades of specialized production, our facility integrates high-precision continuous cold-roll forming, robotic automated welding lines, and electrostatic thermosetting powder coating processes to deliver industrial racking systems optimized for global distribution networks.
Engineering Benchmark: Material Properties & Structural Specifications
To evaluate China rack storage shelves factories effectively, procurement directors and structural engineers must examine raw material selection, profile geometry, and yield strengths. The table below outlines our enterprise engineering benchmarks:
| Structural Parameter | Standard Commercial Grade | Enterprise Heavy-Duty Grade (Our OEM Spec) | Engineering Benefit & Information Gain |
|---|---|---|---|
| Steel Grade & Yield Strength | Q195 / Q235 Common Carbon Steel | Q235B / Q355B High-Tensile Structural Steel | Increases ultimate tensile load bearing capacity by up to 35% under peak stress. |
| Upright Column Pitch | 75 mm / 76.2 mm fixed pitch | 50 mm / 75 mm precision pitch adjustment | Allows tighter beam spacing, optimizing vertical cubic storage density. |
| Coating Technology | Basic liquid paint or standard spray | AkzoNobel thermosetting epoxy powder coating | Passes 500+ hours neutral salt spray test (ISO 9227); high impact & scratch resistance. |
| Structural Design Compliance | Basic static calculations | FEM 10.2.02, RMI (USA), ABNT NBR 15524 (BR) | Full Finite Element Analysis (FEA) safety modeling for seismic and wind load dynamic safety. |
| Beam Locking Mechanism | 2-Hook standard friction pins | 3 or 4-Hook safety automatic drop-lock connectors | Prevents accidental beam dislodgement during high-speed forklift operation. |
| Deflection Ratio Allowance | L / 150 deflection limit | Strict L / 200 or L / 300 structural beam rating | Minimizes structural sag under max dynamic capacity, preserving automated picker tolerances. |
Deep Categorical Breakdown of Heavy-Duty Racking Architecture
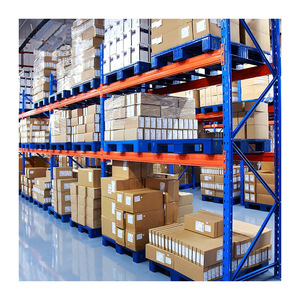
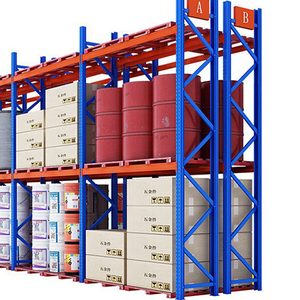
1. Selective Pallet Racking Systems
The standard benchmark for 100% immediate SKU accessibility. Configured with adjustable box beams or step beams, selective pallet racking accommodates any pallet size or MHE type. Ideal for fast-moving consumer goods (FMCG), third-party logistics (3PL), and multi-SKU retail fulfillment hubs.
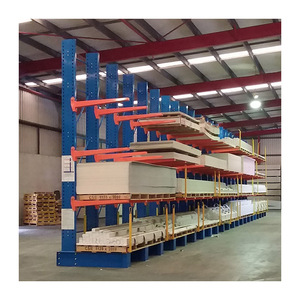
2. Cantilever Storage Racks for Long Goods
Specially engineered for non-palletized, long-span structural materials including steel pipes, aluminum extrusions, timber planks, and plastic tubing. Features continuous horizontal arms mounted on heavy-duty upright columns with adjustable pitch, eliminating front vertical aisle obstructions.
3. Heavy Mold & Die Drawer Storage Systems
Specifically designed for heavy machinery factories, plastic injection plants, and stamping facilities. Equipped with 3-tier slide-out drawer trays, each level handles up to 2,000kg to 5,000kg. Integrated top monorail hoist systems facilitate effortless mechanical die placement.
4. Drive-In & Drive-Through High-Density Systems
Maximizes floor footprint utilization up to 85% by eliminating operational aisles. Forklifts drive directly into storage lanes supported by continuous cantilever pallet rails. Ideal for homogeneous bulk cargo, cold-chain storage facilities, and agricultural seasonal inventories using LIFO/FIFO logistics.
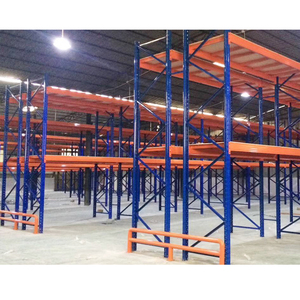
5. Multi-Tier Rack-Supported Mezzanine Systems
Utilizes vertical building height to create 2-tier or 3-tier operational floors. Combined with heavy-duty structural columns and steel grating decks, mezzanine floors double or triple usable area without civil building extension permits—perfect for manual e-commerce pick modules.
6. Long Span Heavy Duty Metal Shelving
Designed for medium to heavy hand-loaded items weighing between 200kg to 800kg per level. Features boltless beam connection mechanisms, wire mesh decking, or steel shelves, enabling rapid assembly and modular expansion across spare parts centers and maintenance workshops.
Why Enterprise B2B Buyers Partner With Our China Factory
With over 18 years of specialized manufacturing experience since 2005, our production base operates as a premier exporter of industrial racking. Our 120+ team of certified structural engineers, international trade specialists, and QA auditors ensures every export shipment meets rigorous global benchmarks.
Advanced Automated Manufacturing Infrastructure
Our facility houses 16 continuous automated roll-forming lines, robotic laser cutting units, and automatic continuous welding cells. This machinery guarantees strict dimensional tolerances (+/- 0.5mm) on profile punchings, ensuring flawless field installation.
Comprehensive Quality Assurance & Certifications
Certified under ISO 9001 quality management systems, our products comply with European CE safety standards, Japanese JIS standards, and South American ABNT NBR 15524 regulations. Every batch undergoes raw material coil testing and weld seam inspection.
Custom OEM/ODM CAD & 3D Structural Modeling
We provide zero-cost preliminary warehouse floor plan designs. By reviewing your CAD DWG drawings, pallet weight profiles, clear ceiling height, and forklift turning radiuses, our engineering team delivers optimized rack layouts and FEA structural safety reports.
Global Export Logistics & Port Readiness
Exporting annually over $16M USD in heavy racking systems, we optimize container loading (20GP / 40HQ) with heavy-duty steel bundling, protective film wrapping, and timber dunnage to eliminate transit damage to major global ports like Santos, Rotterdam, Hamburg, and Long Beach.
Future Procurement Trends: Industry Evolution (2025–2030)
The industrial storage equipment sector is undergoing rapid technological transformation. When sourcing from China racking factories, global procurement managers should align with these emerging technological and operational trends:
1. Integration with AS/RS and Automated Four-Way Radio Shuttles: Conventional static racking is increasingly giving way to shuttle-ready structural frames. High-density radio shuttle racks allow autonomous battery-powered shuttles to navigate inside storage tunnels, driving higher pallet throughput and reducing operator labor costs.
2. High-Strength Cold-Formed Steel Profiles (Q355B & Beyond): To minimize total structural weight while maintaining static load integrity, advanced factories utilize higher yield strength micro-alloyed steels. This permits lighter upright profile gauges without compromising load capacity, reducing raw material utilization and international ocean freight expenses.
3. Eco-Friendly Thermosetting Finishes & Corrosion Resistance: Environmental regulations are driving factories to switch to zero-VOC, heavy-metal-free powder coatings. Furthermore, hot-dip galvanized (HDG) rack finishes are expanding rapidly into cold-storage, chemical, and humid coastal warehouse environments due to their 20+ year rust-free durability.
4. Smart Sensors & Real-Time Structural Health Monitoring: Next-generation rack structures are integrating IoT impact sensors on upright column protectors. These sensors log forklift collision impacts in real time, alerting safety managers to structural deformation risks before catastrophic frame collapses occur.
Frequently Asked Questions (Sourcing & Technical FAQ)
Accelerate Your Warehouse Capacity With Direct China Factory Engineering
Send your building floor plan, storage requirements, or product specifications to our technical engineering team. Receive customized 2D/3D layout drawings and competitive factory-direct pricing within 24 hours.
Inquire Now