Featured Industrial Pallet Racking Systems
Direct-from-factory high-density warehouse solutions certified to FEM, RMI, and ISO international safety codes.
1. Executive Sourcing Analysis: The Ecosystem of Chinese Pallet Racking Manufacturers
In the contemporary global logistics landscape, storage infrastructure represents a critical capital investment that directly influences supply chain throughput, inventory velocity, and operational safety. As industrial hubs expand across North America, Europe, Latin America, and Southeast Asia, procurement directors increasingly turn to China’s premier pallet racking suppliers to secure high-tensile structural steel storage systems that harmonize engineering rigor with capital efficiency.
China’s industrial racking manufacturing sector has evolved from basic component rolling to sophisticated structural engineering. Top-tier Chinese manufacturers operate advanced continuous automated roll-forming lines, robotic welding cells, and eco-friendly electrostatic powder-coating facilities. This technological transition ensures that industrial heavy-duty pallet racks produced by leading suppliers comply strictly with international structural design codes, including FEM 10.2.02 (European Federation of Materials Handling), ANSI MH16.1 (Specifications for the Design, Testing and Utilization of Industrial Steel Storage Racking by RMI), AS4084-2012 (Australian Standard for Steel Storage Racking), and ABNT NBR 15524 (Brazilian Standard).
High-Tensile Cold-Rolled Steel
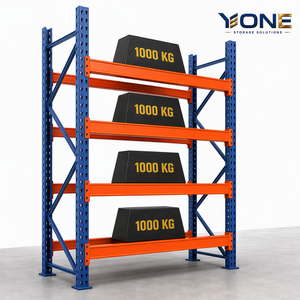
Structural profiles utilize certified Q235B and Q355B (equivalent to S235JR and S355JR structural steel grades), delivering optimized strength-to-weight ratios capable of supporting single-bay load capacities exceeding 45,000 kg.
Precision Automated Roll-Forming
Computer-controlled multi-station cold-rolling mills ensure ultra-tight dimensional tolerances (±0.5 mm), guaranteeing exact beam connector engagements and uniform upright pitch configurations across multi-tier structures.
Surface Treatment & Corrosion Resistance
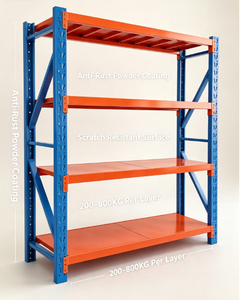
Multi-stage automatic degreasing, iron-phosphating pre-treatment, and thermosetting epoxy-polyester powder coating (60–80 μm thickness) provide maximum resistance to impact, chemical exposure, and humidity.
2. Structural Metallurgy & Global Compliance Framework
A primary factor distinguishing top-tier Chinese manufacturers from budget fabricators is structural engineering integrity. Heavy-duty pallet racking systems must withstand static live loads, dynamic forklift impacts, frame column eccentricities, and seismic forces. Structural integrity relies heavily on raw material metallurgy and profile geometry design.
Steel Grade Standard & Engineering Matrix
The structural performance of pallet racking uprights and load-bearing box beams depends on the yield strength ($f_y$) and ultimate tensile strength ($f_u$) of the raw steel coil. Leading Chinese suppliers source prime structural steel directly from state-owned steel conglomerates (such as Baosteel, Shougang Group, and Ansteel), ensuring full mill test certification (MTC) for every production lot.
| Chinese Steel Grade | International Equivalent | Yield Strength ($f_y$ Min) | Tensile Strength ($f_u$) | Primary Racking Component Application |
|---|---|---|---|---|
| Q235B | ASTM A36 / EN S235JR | 235 MPa | 370 – 500 MPa | Standard load beams, wire mesh decking, shelf plates, row spacers |
| Q355B | ASTM A572 Gr 50 / EN S355JR | 355 MPa | 470 – 630 MPa | Heavy-duty high-bay upright columns, heavy rack-supported mezzanines |
| Q460 High-Strength | EN S460 / Weldox 460 | 460 MPa | 550 – 720 MPa | Ultra-high-bay ASRS upright frames (15m–30m tall structures) |
| Pre-Galvanized (Z275) | EN 10346 DX51D+Z | 250 MPa | 330 – 420 MPa | Cold storage facilities, outdoor cantilever racks, agricultural stores |
To meet strict international standards, upright frames undergo finite element analysis (FEA) to simulate complex axial loading, torsional-flexural buckling, and second-order P-Delta ($\text{P-}\Delta$) structural effects. Beam-to-column connections are engineered with multi-claw forged steel connectors featuring automatic spring-safety locks to prevent accidental beam displacement during high-speed forklift operation.
3. Taxonomy of Advanced Industrial Pallet Racking Systems
Every warehouse facility presents unique spatial geometry, floor load constraints, SKU turnover velocities, and material handling equipment dynamics. Top Chinese manufacturers design and supply a broad spectrum of heavy-duty pallet racking configurations:
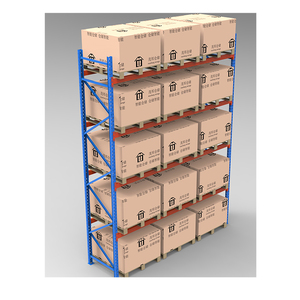
Selective Pallet Racking
Pallet Accessibility: 100% Direct Access
Storage Density: Moderate (35–40% floor utilization)
Best For: High-SKU diversity, fast FMCG fulfillment, distribution hubs requiring instant stock picking access.
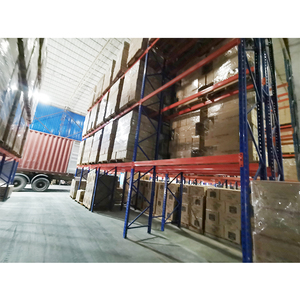
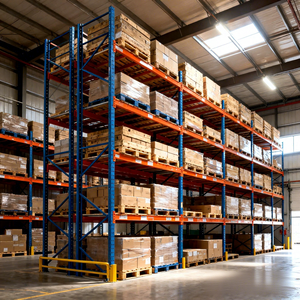
Configured with single or double-deep rows, selective pallet racking represents the most versatile and cost-effective warehouse storage architecture worldwide.
Drive-In & Drive-Through Racking
Pallet Accessibility: LIFO (Drive-In) / FIFO (Drive-Through)
Storage Density: High (65–75% floor utilization)
Best For: Homogeneous bulk goods, cold storage logistics, food & beverage seasonal inventory.
Eliminates operating aisles by allowing forklifts to drive directly into storage lanes, placing pallets on continuous side support rails.
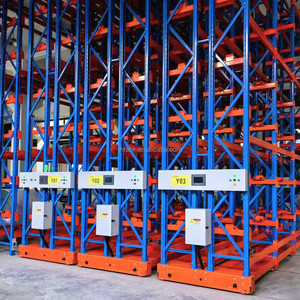
Electric Mobile Pallet Racking (MOVO)
Pallet Accessibility: 100% On-Demand Access
Storage Density: Ultra-High (80–85% floor utilization)
Best For: High-cost refrigerated warehouses and pharmaceutical cold chains.
Pallet racks are mounted on guided electric mobile bases that travel along embedded floor tracks, opening a single operational aisle via remote control or PLC automation.
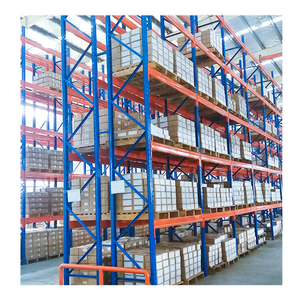
High-Rise Beam & VNA Racking
Pallet Accessibility: 100% Access via Turret Trucks
Storage Height: 10m to 18m Tall Bays
Best For: Modern high-ceiling logistics centers seeking maximum cubic volumetric efficiency.
Very Narrow Aisle (VNA) systems compress aisle widths down to 1.5–1.8 meters, dramatically increasing vertical capacity while maintaining 100% selectivity.
Cantilever Heavy-Duty Racking
Pallet Accessibility: Unobstructed Frontal Access
Load Capacity: 500 kg to 3,000 kg per arm
Best For: Storing long, bulky items such as steel pipes, timber, aluminum extrusions, and PVC conduits.
Features freestanding vertical columns with extended support arms, completely eliminating front column structural interference.
Rack-Supported Mezzanine Systems
Pallet Accessibility: Multi-Tier Hand-Picking & Pallet Loading
Floor Area Multiplier: 200% to 300% expansion
Best For: E-commerce fulfillment hubs, spare parts archives, and manual order assembly zones.
Utilizes racking components as structural support columns to construct integrated multi-level flooring decks equipped with steel staircases, catwalks, and safety handrails.
4. Future Sourcing & Technology Trends in Industrial Racking (2025–2030)
The global material handling industry is undergoing a structural shift driven by automation, sustainability, and real-time inventory tracking. Procurement managers must evaluate how pallet racking investments align with upcoming technological changes over the next decade:
AS/RS & AMR Integration
Future-ready pallet racking is increasingly optimized for Autonomous Mobile Robots (AMRs), Automated Guided Vehicles (AGVs), and stacker cranes. Manufacturing tolerances for high-bay racking systems are shrinking to millimetric precision to ensure seamless automated positioning and optical sensor alignment.
Smart Sensor Monitoring
Leading tier-1 suppliers are testing smart racking structural monitoring systems. Wireless IoT strain-gauge sensors embedded in critical upright columns provide real-time telemetry on structural deflection, accidental forklift impact forces, and load balance, alerting facility managers to potential structural hazards.
Green Steel & Zero-VOC Coatings
Environmental, Social, and Governance (ESG) criteria are altering global supply chains. Top Chinese factories are adopting decarbonized green steel coils produced via hydrogen direct reduction (DRI) alongside zero-VOC thermosetting powder coatings to minimize the carbon footprint of structural installations.
5. Enterprise Manufacturing Rigor & Global Logistics Capabilities
Founded in 2005, our manufacturing enterprise has established a global footprint as a premier industrial pallet racking OEM/ODM supplier. Operating with over 120 dedicated structural engineers, production technicians, and international logistics coordinators, our facility generates an annual export volume exceeding US$16 Million across North America, South America (including full coverage across all 26 states of Brazil), Europe, the Middle East, and Asia-Pacific.
4-Stage Quality Assurance Protocol
To maintain an unblemished structural safety record across international installations, every production batch adheres to a standardized Quality Control (QC) framework:
Spectral analysis of steel coil chemical composition, tensile yield testing, and ultrasonic thickness verification prior to roll forming.
Continuous optical laser checks during profile cold-rolling to ensure straightness, pitch accuracy, and hole punch geometry within ±0.3 mm.
Robotic MIG/MAG welding joints undergo dye-penetrant inspection and destructive shear testing to guarantee full structural penetration.
500-hour neutral salt spray (NSS) testing, cross-hatch paint adhesion checks, and digital coating thickness measurements (60–80 μm).
Export Packing & Ocean Freight Logistics
Overseas transport presents severe environmental risks, including sea-water corrosion, container moisture condensation, and dynamic transit vibration. Our specialized export packing methodology incorporates steel strapping, heavy-duty corrugated edge protectors, plastic stretch wrapping, and custom wooden dunnage to protect structural components during ocean transit to key international ports (including Santos, Paranaguá, Itajaí, Hamburg, Rotterdam, Long Beach, and Dubai).
6. Frequently Asked Questions (FAQ) for Global Procurement Officers
Addressing structural engineering, international compliance, lead times, and customization options when sourcing pallet racking systems from China.
Request a Custom Engineering Design & Factory Direct Quote
Submit your warehouse floor plans, clear building height, pallet specifications, and target storage capacities. Our engineering team will return a complete CAD layout and structural quotation within 24 business hours.